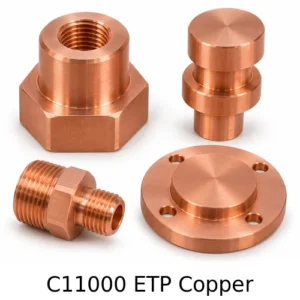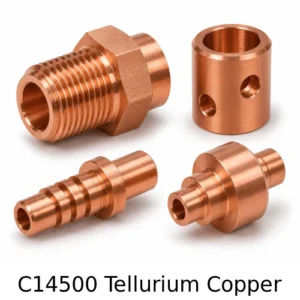


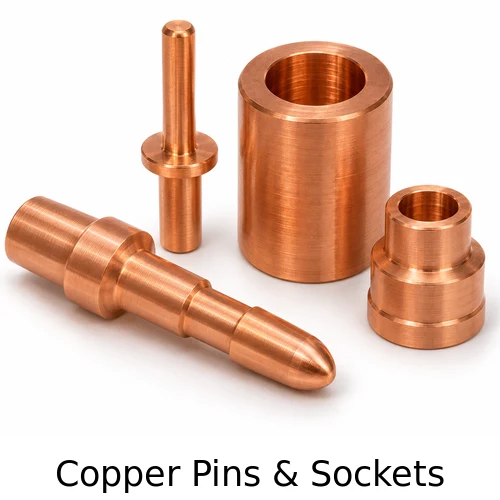
Copper Electrical Contact Pins and Turned Sockets
Rate: US$19.50 per kg
A turned contact pin and its mating socket operate as a pair. The drawing has to establish the lead-in, the working contact zone and the mechanical stop so the contact area develops at the intended depth. Conex Screws reviews solid pins, stepped conductive posts and precision turned socket bodies from customer drawings. Buyers can supply separate part drawings and an assembly cross-section showing the contact stack. Where the socket receives a separate spring element, identify whether the quotation is for the machined body alone or for additional supplied elements.
The pin’s major diameter is only one input to a stable connection. A bore with taper or a burr can damage plating during assembly and increase insertion force. Poor alignment can concentrate load at the entry and keep the working surfaces from overlapping as intended. Specify measurements over the actual working length and account for coating on both mating members. If finished contact resistance or cycle life is a requirement, define it in an assembly test plan with the intended current, load and environment.
Pin and socket configurations
| Part or characteristic | Drawing and application details | Inspection and quoting considerations |
|---|---|---|
| Straight solid contact pin | Locate the working diameter and show the rounded or chamfered lead-in separately from the overall length. | Use a suitable diameter method at multiple points in the working zone when taper or barrel shape affects fit. |
| Stepped pin with mounting shoulder | State whether the shoulder locates the pin in insulation, carries a terminal clamp or provides the mechanical insertion stop. | Establish the shoulder position and working diameter from functional datums. Review corner radius against the mating recess. |
| Bored socket body | Define the inside bore, working contact depth and clearance behind the mating pin tip. | An internal gauge can check size. Where a step or taper affects assembly, inspect it independently and show where the gauge must engage. |
| Flanged contact receptacle | Define the mounting flange seating surface and how the receptacle is held in the housing. | Check flange thickness, face runout and whether the housing bore locates the body or leaves radial float. |
| Slotted socket body | Specify slit width, location and edge condition if the slots are part of the design. | Review the production process and assembly requirements before specifying spring action. Contact force depends on material and the full mechanical design. |
Measurements that affect mating
| Part or characteristic | Drawing and application details | Inspection and quoting considerations |
|---|---|---|
| Insertion and extraction | State whether the criterion applies to a new pair, a cycled pair or a pair conditioned at a specified temperature. | Agree on travel speed, stroke and the reference mate. Keep the mechanical fixture from introducing a side load. |
| Contact resistance | Identify current injection and voltage sensing locations along with test current and surface preparation. | Separate bulk conductor resistance from interface behavior by defining exactly where the measurement spans. |
| Plating thickness and wear | State coating, underlayer if required and the plated contact area on both mating parts. | Calculate the allowance from finished dimensions and inspect after plating. Include the cycle count and wear limit if the application needs it. |
| Pin alignment | Dimension relevant diameters and runout relative to the installed locating feature. | Verify the engagement path with the actual mating components if the housing constrains alignment and float. |
| Cleanliness in blind bores | Identify oil, particle and residue limits for the mating zone when assembly performance depends on them. | Include a check for trapped chips and agree the cleaning and packaging method for small bores. |
Engineering questions for the first article
What if the connector uses a separate spring band?
Provide the groove form, installed spring position and a section view of the complete socket assembly. Clarify the source of the spring band and the method to check retention. The turned body carries dimensional requirements, while the assembled connector establishes mating and electrical performance.
Should a pin and socket use the same copper grade?
The pair can use different approved materials depending on conduction, wear, machinability and mechanical loading. The equipment designer decides whether the material combination supports the required service. Give each component its own grade and temper on the print and identify any approved alternatives.
What is the difference between nominal bore and usable contact depth?
Nominal bore states a diameter. Usable depth describes the axial length over which the intended contact occurs. Entrance chamfers, drill point geometry and reliefs can shorten that zone. Section the geometry on the print and dimension the working zone from the mating face.
Can you inspect the pins and sockets as an assembly?
A matched sample or inspection fixture can be quoted when the customer supplies the acceptance method and identifies the critical conditions. Define insertion travel, force limits and the environmental state as applicable. Record dimensional results for the component drawing separately from assembly results.
An illustrative pin-and-socket fit calculation
Consider a finished pin measuring 5.980 to 5.990 mm and a finished solid socket bore measuring 6.000 to 6.015 mm. The theoretical diametral clearance at the two extremes is 0.010 to 0.035 mm, assuming cylindrical parts aligned on one axis and ignoring position, form and temperature effects. These example values explain tolerance analysis. They are not a fit recommendation for a production connector or a specification for a spring-contact system.
If both components were measured before plating and each mating surface received a uniform 5 micrometre deposit, the pin would grow by 0.010 mm in diameter while the bore would shrink by 0.010 mm. In the simple example, the clearances would each fall by 0.020 mm. The smallest clearance would become a nominal 0.010 mm interference. Give the finished size and describe coating on both parts early enough to plan machining and inspection. Actual deposits can vary around edges or inside deep recesses.
Define the zones of a contact pin
Divide the length into entry, working contact, mounting and exit or relief zones. The entry radius or chamfer guides engagement. The working zone defines the intended contact length. The mounting zone retains the pin and can carry a thread, groove or press-fit diameter. A relief or reduced tip can provide clearance, provided it does not reduce the length required for engagement. Identify where coatings begin and end, especially if the mating interface crosses a coating transition.
If the contact is supported in insulation or located by a housing, share the locating fit. Misalignment can make one side of the pin carry more load, which can change insertion force and wear. Check relevant pin diameters at multiple sections and agree a runout or position check where the assembly requires it. With very small contacts, confirm that measurement force and fixture alignment do not bias readings or mark the surface.
Develop an assembly validation plan
Insertion force and extraction force describe different parts of the mating cycle. Identify the target travel speed, contact condition, cleaning procedure, temperature and number of cycles before acceptance. Decide whether the highest measured value, force at a given depth or average over a travel segment matters. The reference counterpart should be controlled because a worn or damaged mating sample can give different readings even when the turned components are consistent.
Electrical validation can include a defined resistance reading under a prescribed engagement and load. Provide the current and voltage sensing positions, the allowed temperature range and any dwell period. For a cycle test, state when measurements are required and whether a change from initial resistance or an absolute value controls acceptance. The equipment designer defines current rating, force and lifetime. The machining quotation can separately identify which agreed dimensional, coating and assembly checks are included.
Identify the connector supplied
A quote for a turned copper socket body covers the specified metal geometry and agreed finishing. A complete connector assembly can include insulating bodies, crimp features, springs or separately purchased elements. Provide a bill of materials to separate the turned part from any assembly scope. For contact sets, identify whether pairing or independent interchangeability is required.
How to prepare a drawing for quotation
Send a dimensioned PDF for acceptance and a STEP model for geometry review when available. Identify the current revision on both files. The PDF should distinguish basic, reference and toleranced dimensions, specify units and define precedence when the model and drawing disagree. Share the assembly context if the finished part seats against an insulator, mates with another copper piece or passes through an enclosure. The most valuable information is usually a section through the working axis and a note identifying the features that govern acceptance at receiving.
Mark the expected order quantity, lot size and annual demand separately. Production tooling, inspection and stock planning depend on how the demand is released. A batch of samples can qualify geometry before the full release. If the drawing changes between a sample and production order, state whether the earlier inspection report still applies and list the features affected by the change. Include any quality clauses that carry over to later releases.
Choose the stock specification and condition
A copper grade is a material designation. It does not specify all of the attributes of the starting stock. State the form, temper, material specification and revision required by the contract. Where the drawing cites ASTM B187/B187M for copper rod, bar or shapes, confirm that the grade and stock form are covered by the selected edition and scope. If stock is approved to a different standard, request engineering disposition before material is ordered. Separately identify the requirements for the finished component, including dimensional checks, coating and packaging.
A material test report is most useful when the receiving team can map it to the parts in a container. If traceability is contractual, define whether it must be maintained by heat, manufacturing lot or individual piece, and how identification will be applied. A bag or carton label can protect working surfaces from marking. A permanent stamp needs an approved location away from mating faces, thin walls and tight diameters.
Set up the turning sequence around the working interface
Turned features that share an axis may benefit from production in one setup. A long bore, slot or radial hole can still require an additional operation. Establish which relationships drive the setup before the machining plan is frozen. If a part must transfer to another chuck or a separate fixture, identify the gripping zone and the surface that re-establishes the location. Check whether a previously finished section must be protected against fixture marks.
A part drawing can leave the machining sequence to the supplier while preserving requirements for the result. For qualification, ask the supplier to explain how the operation sequence protects critical faces and how it will respond when tools wear or stock changes. Where sequence is contractual because of an approved special process, put that requirement on the purchase order and identify the conditions under which a change needs customer approval.
Specify bore geometry and tool access
On a blind hole, distinguish total drilled depth from the depth of full cylindrical diameter. If the hole contains a thread, specify full-form thread depth separately from the depth of drill point and thread runout. A counterbore or spotface should have its own dimension from the reference face. Deep narrow passages need sufficient access for measurement as well as for machining. If the application accepts the natural drill point, that allowance can help simplify inspection and production.
For a through bore, give the edge requirement at both ends. A raised burr on the exit face can prevent the part from seating and skew an assembly. If a radial passage intersects the axial bore, establish where the edges may be broken and which intersection surfaces must remain clear. Inspection may combine measurement of the passage with a visual or functional check for blocked flow or snagging, depending on the application.
Use thread callouts a buyer and inspector can verify
Use the thread series, nominal size, pitch and class from the drawing. Unified inch callouts can refer to ASME B1.1 as applicable. A metric M-profile callout uses a metric diameter and pitch and its own tolerance designation. State left-hand thread explicitly when required. For an unusual thread, supply the mating drawing or master and the acceptance method. A drawing that shows only nominal diameter may leave incompatible threads looking interchangeable to a buyer.
Define usable engagement, the clearance at the end and the entry edge. On a blind tapped part, specify how much full-form thread is needed ahead of the runout. On an external stud-like feature, verify that a relief groove does not remove a length needed for engagement. Standard thread gauges check the aspects of the thread covered by their design. Where an installed shoulder or a mating member with its own runout limits travel, add a functional fit check to the inspection plan.
Compare turned surfaces, finish and edge treatment
The surface roughness requirement should identify the parameter, units and working area. When traces can run in more than one direction, specify the direction relevant to the function and the method if it is important for repeatability. Compare the desired finish with what the actual bearing surface or bore can accommodate. A small annular contact pad may leave limited space for an instrument trace, so agree the method before production.
Define where burrs are unacceptable and where edge rounding is constrained. A blanket edge break may be inappropriate on small grooves or edges that establish a working length. Show these as exceptions and identify safe handling edges where a normal chamfer is acceptable. Agree whether small surface marks are cosmetic or restricted by a functional requirement. A photographic limit sample can help clarify a finish specification when visual acceptance matters.
Plan coating around the finished part
Tin, silver and nickel can serve different functions. Specify the coating and any underlayer, thickness and areas to cover on the drawing. Call out surfaces that need masking, any limits on buildup or bridging, and areas used for rack contact if a witness mark matters. Report material and coating requirements separately so the ordering team can distinguish the base copper from the final surface. When the intended process is still being selected, describe the application and ask for an engineering review.
In a simple concentric bore with a uniform deposit on both opposing walls, a coating of thickness t on each wall reduces the diameter by approximately 2t. A corresponding outside diameter increases by about 2t. This geometric estimate assumes uniform coverage and simple cylindrical surfaces. A deep blind hole can plate unevenly, and threads require separate treatment of flank geometry and gauge fit. Verify the finished fit using the inspection method agreed for the drawing.
Agree how critical dimensions will be measured
The inspector needs the same functional datums as the design and assembly teams. Specify what establishes the axis, the face from which axial distances are measured and any feature that clocks a slot or hole. A datum setup should support the part without distorting it. For short or slender features, identify a practical checking method before committing to a tight dimensional tolerance. A dimension that can be machined reliably still needs a method that can distinguish conforming parts.
External diameters can be measured at selected planes, while bores may require plug gauges, internal measuring instruments or coordinate measurements. A go gauge confirms an acceptance condition within its design. It does not report the full bore profile. If taper, ovality, position or axial variation matters, put that geometric requirement on the drawing and agree how to check it. Document the inspection condition when temperature, measuring force or fixturing can change the readings.
First article and ongoing inspection
A first article is most useful when it comes from the intended production material and process route. Ask for a marked-up drawing with numbered characteristics and a report showing actual values for the agreed dimensional features. Give a separate row to any functional test, material verification or coating acceptance criterion. Review the lot certificate and finished inspection together so the identified sample can be tied to its stock and operation history.
Agree sampling and records before production. Identify any features subject to complete inspection, any dimensions to record at process intervals and the method for addressing a suspect batch. If process capability is requested, define the study conditions and the minimum data set. A first article shows an inspected sample at a point in time. Ongoing records and change control show whether the agreed process continues to deliver the same features during repeat orders.
Receiving and handling of machined copper parts
Decide how parts are cleaned after machining and after any coating. Bores, slots, blind recesses and intersecting holes can retain chips or processing fluid. Give a cleanliness test or an acceptance sample when the allowable condition is important. Define whether the supplier may use corrosion protection or whether the component will go directly into a customer cleaning, soldering or assembly step. Incompatible protective products can create additional preparation work at receiving.
Protect dimensions that are easy to mark or distort. Separate sharp projections from thin walls and keep the working faces from rubbing against one another. Discuss trays, dividers, individual sleeves or simple bulk packaging in light of the size, surface condition and handling route. Identify the lot, drawing revision, order number and quantity on the outer label when requested. Where the parts are supplied in groups for a matched assembly, give each group a distinct identifier.
Common RFQ questions
Can Conex Screws quote from a sample?
A physical sample can help identify the machining route, mating conditions and finish. Supply a drawing or approve a controlled drawing before production. Surface measurements on the sample may include wear, distortion or coating, so identify the accepted nominal values and state whether a replacement part must mate with legacy hardware.
Can I request both metric and inch information?
Yes. Use one unit system as the controlling dimension set and mark the other as reference where appropriate. An exact unit conversion can produce a precision that the original tolerance did not intend. Keep the thread family in its native designation. If the product goes into a mixed-unit assembly, share the mating drawing with the enquiry.
How are tolerances and lead time confirmed?
Review is based on grade, part geometry, tolerances, inspection, lot size and the stock or tooling needed for the order. Highlight the dimensions tied to assembly or electrical performance. Conex Screws can then review measurable acceptance methods, production sequence and lead time with the buyer at quotation.
How does the per-kilogram rate relate to ordering?
The listed rate for this product family is US$19.50 per kilogram. Send the drawing and requested quantity for a written quote that identifies the order basis, finish, inspection and shipping terms. If your purchasing system orders individual pieces, request the agreed piece-weight basis and price presentation for the quotation.
Can I specify a material grade different from the examples?
State the UNS designation, specification and temper and provide the target application. Quote review can check grade and stock availability, cutting access and inspection. Procurement should approve the exact designation against the drawing before any material is released.
Which checks apply before and after plating?
Use before-coating checks where they control machining or establish a baseline. Set finished-part acceptance against the agreed drawing and functional gauges. Where access is limited, agree coating measurement locations and test frequency at quote stage. Provide an approved mate for assembly-sensitive interfaces when useful.
What should a quote package include?
Provide the product drawing, revision, part quantity, target delivery, material grade and temper, critical tolerances, finish, packaging and any required reports. Include the mating drawing or assembly section if available. Attach any first article forms and identify requirements that have to be agreed before materials are procured.
Turn an assembly requirement into an inspection characteristic
Start with a sentence describing the risk. A part that stops short at assembly, rocks under a clamp or loses engagement during handling needs a different check in each case. Identify the feature in the drawing section that controls the outcome. Write its acceptance as a measurement with a datum or as a test with a controlled mating condition. Avoid a note that relies only on interpretation, such as asking for a good fit, when the requirement can be described in a drawing or test plan.
Create a short list of characteristics that govern release. Review them with the receiving team so the supplier knows which actual values and documents to include. A first article can document the relationship between related features, and ongoing checks can focus on the measurements likely to change during production. If a tolerance is changed in the drawing, record which master sample or gauge revision applies. When the fit depends on a downstream operation, agree whether the receiving inspection verifies an intermediate condition or the finished assembly.
Manufacturing and purchasing checklist
Before ordering, confirm that the drawing names the component and clearly identifies the part revision. Verify that the quotation records the same material and the same delivery condition. Ask for an approved sample or dimensional report if the geometry is new, if a new stock size must be sourced or if the same part number was previously ordered with a different finish. Include an approved deviation on the order when engineering has accepted an exception. Identify the point at which approval expires if the deviation applies only to samples.
Set the information required for future reorders. Preserve the drawing number, revision, material requirement and the inspection or packing conditions that define the part. Where samples use a process different from the intended production route, agree what evidence the production process needs before release. Where a surface has multiple requirements, identify their order of precedence and the areas to which they apply. This gives purchasing a repeatable order description and gives the incoming inspector a set of clear checks.
Define the finish and limits for visual acceptance
A finished machined surface may have normal turning marks visible under directional lighting. When appearance affects assembly or end customer acceptance, state the lighting, viewing area and permissible marks, or reference approved samples. On a concealed body, machining marks outside the working area may matter only where they create a burr or change the dimension. On a mating diameter or face, the same marks can affect seating or friction. Set the acceptance area on the drawing and identify any surfaces where contact from packing material is restricted.
Agree how witness marks are handled. A rack contact can leave a small mark after plating, and a fixture can mark a part during transfer. Restrict marks on the functional zone and establish any agreed acceptable areas before the process is approved. Keep the visual limits separate from quantitative checks for dimensions, roughness and coating thickness. When a part is intended to be further machined, specify which surfaces remain on the completed assembly and which are left as extra stock.
Material, thread and product references
- Copper Development Association C11000 data
- Copper Development Association C14500 data
- ASTM copper rod, bar and shapes specification
- ASME Unified inch screw thread standard
Send your drawing to Conex Screws
For a quotation, provide your drawing revision, material designation, finish, order quantity and any inspection documents. Include the mating geometry where fit matters. Conex Screws will review the manufacturing and acceptance requirements with your engineering or purchasing team.
Email your drawing for a quote at sales@conexscrews.com
Explore all Copper Screw Machine Parts and CNC Turned Components